How to Read a Graphite Electrode Specification Sheet
What resistivity, bulk density, bending strength and CTE actually mean on the shop floor — and the two columns buyers routinely overlook.
Read article →Cleaning, alignment, tightening torque and joining timing — plus the most common field mistakes that lead to loose joints and electrode breakage.
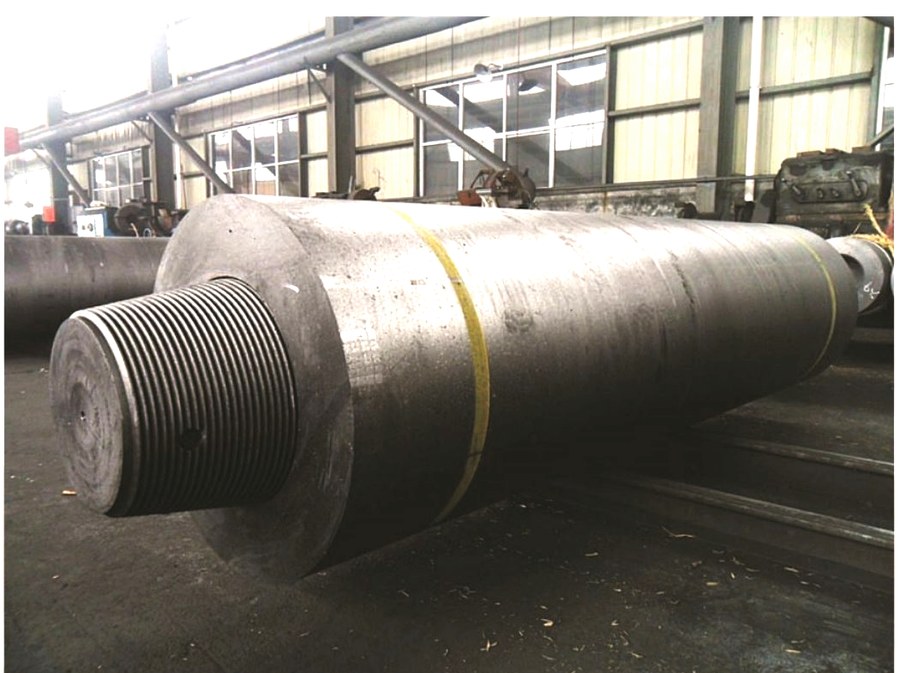
The nipple is the most highly stressed point in an electrode column. In field data, a large share of breakages is nipple-related — and most of those are assembly issues rather than material defects.
Clean: socket, threads and nipple must be free of dust, scale and packaging residue. Foreign material raises contact resistance and creates hot spots.
Inspect: confirm nipple and electrode are the same grade and size, threads are undamaged and the nipple has no cracks. Dry any moisture-affected components per specification before use.
Align: keep the electrode vertical during lifting and lowering, with the two axes as collinear as possible. Eccentric assembly introduces bending moment once current flows.
Use the supplier's specified torque with a dedicated tool — never by feel. Under-torque raises contact resistance, heating and loosening risk; over-torque damages threads and the nipple. Put the value into the SOP and calibrate the tool periodically.
Store electrodes and nipples dry and protected from impact; keep nipples in original packaging until use. Use dedicated lifting gear — never wrap wire rope directly around the electrode body.
| Symptom | Likely cause |
|---|---|
| Red-hot nipple zone | Dirty contact surface, insufficient torque |
| Joint loosens after power-on | Under-torque, worn threads |
| Fracture near nipple | Eccentricity, charge collapse impact, over-torque |
| Column sway | Poor clamping or alignment |
Matched nipples per grade, assembly guidelines and batch inspection data. If your breakage rate is high, send fracture photos and operating parameters — our technical team will help with root-cause analysis.
See the product range for matched sizes, or contact us for the assembly SOP.
Share the diameter, grade, quantity and application, and we'll return a competitive price, a workable technical solution and after-sales support. You're also welcome to reach us directly by phone, email or WhatsApp.
Request a quote →What resistivity, bulk density, bending strength and CTE actually mean on the shop floor — and the two columns buyers routinely overlook.
Read article →
Differences in fixed carbon, sulfur, nitrogen and recovery between graphitized and calcined petroleum coke, with typical steelmaking and foundry applications.
Read article →We have your request. Our sales team will contact you by email, phone or WhatsApp within 24 hours.